
You are using an out of date browser. It may not display this or other websites correctly.
You should upgrade or use an alternative browser.
You should upgrade or use an alternative browser.
What do you 3D print today?
- Thread starter mdcerdan
- Start date


Michael9865
Elite member
Now that is creative! Good luck.
It was not for me, it was for a friend to use. I will let him know that you wished them well.

Keno
Well-known member
Reprinting my PlanePrint Big Bobber, the first one was too heavy & heat warped the wings. Trying out 3D Fuel PLA-Pro & printing at 230c to print .35 mm wall thickness, this maybe also a little heavy but manual has weight for one wing section is 68g & my print came in at 48g we see what happens. I am hoping the 3D fuel PRO has a little better heat resistant spec to helps with warping problem in the sun's heat, we'll still have keep it in the shade when not flying. I tried to anneal it but not a good idea as it became brittle. The print looks much better than LW-PLA as this print has much more detail but still like to work with LW-PLA.
Sorry for the thick measurement. I think in inches not mm
Sorry for the thick measurement. I think in inches not mm
Last edited:

Flightspeed
Convicted Necroposter
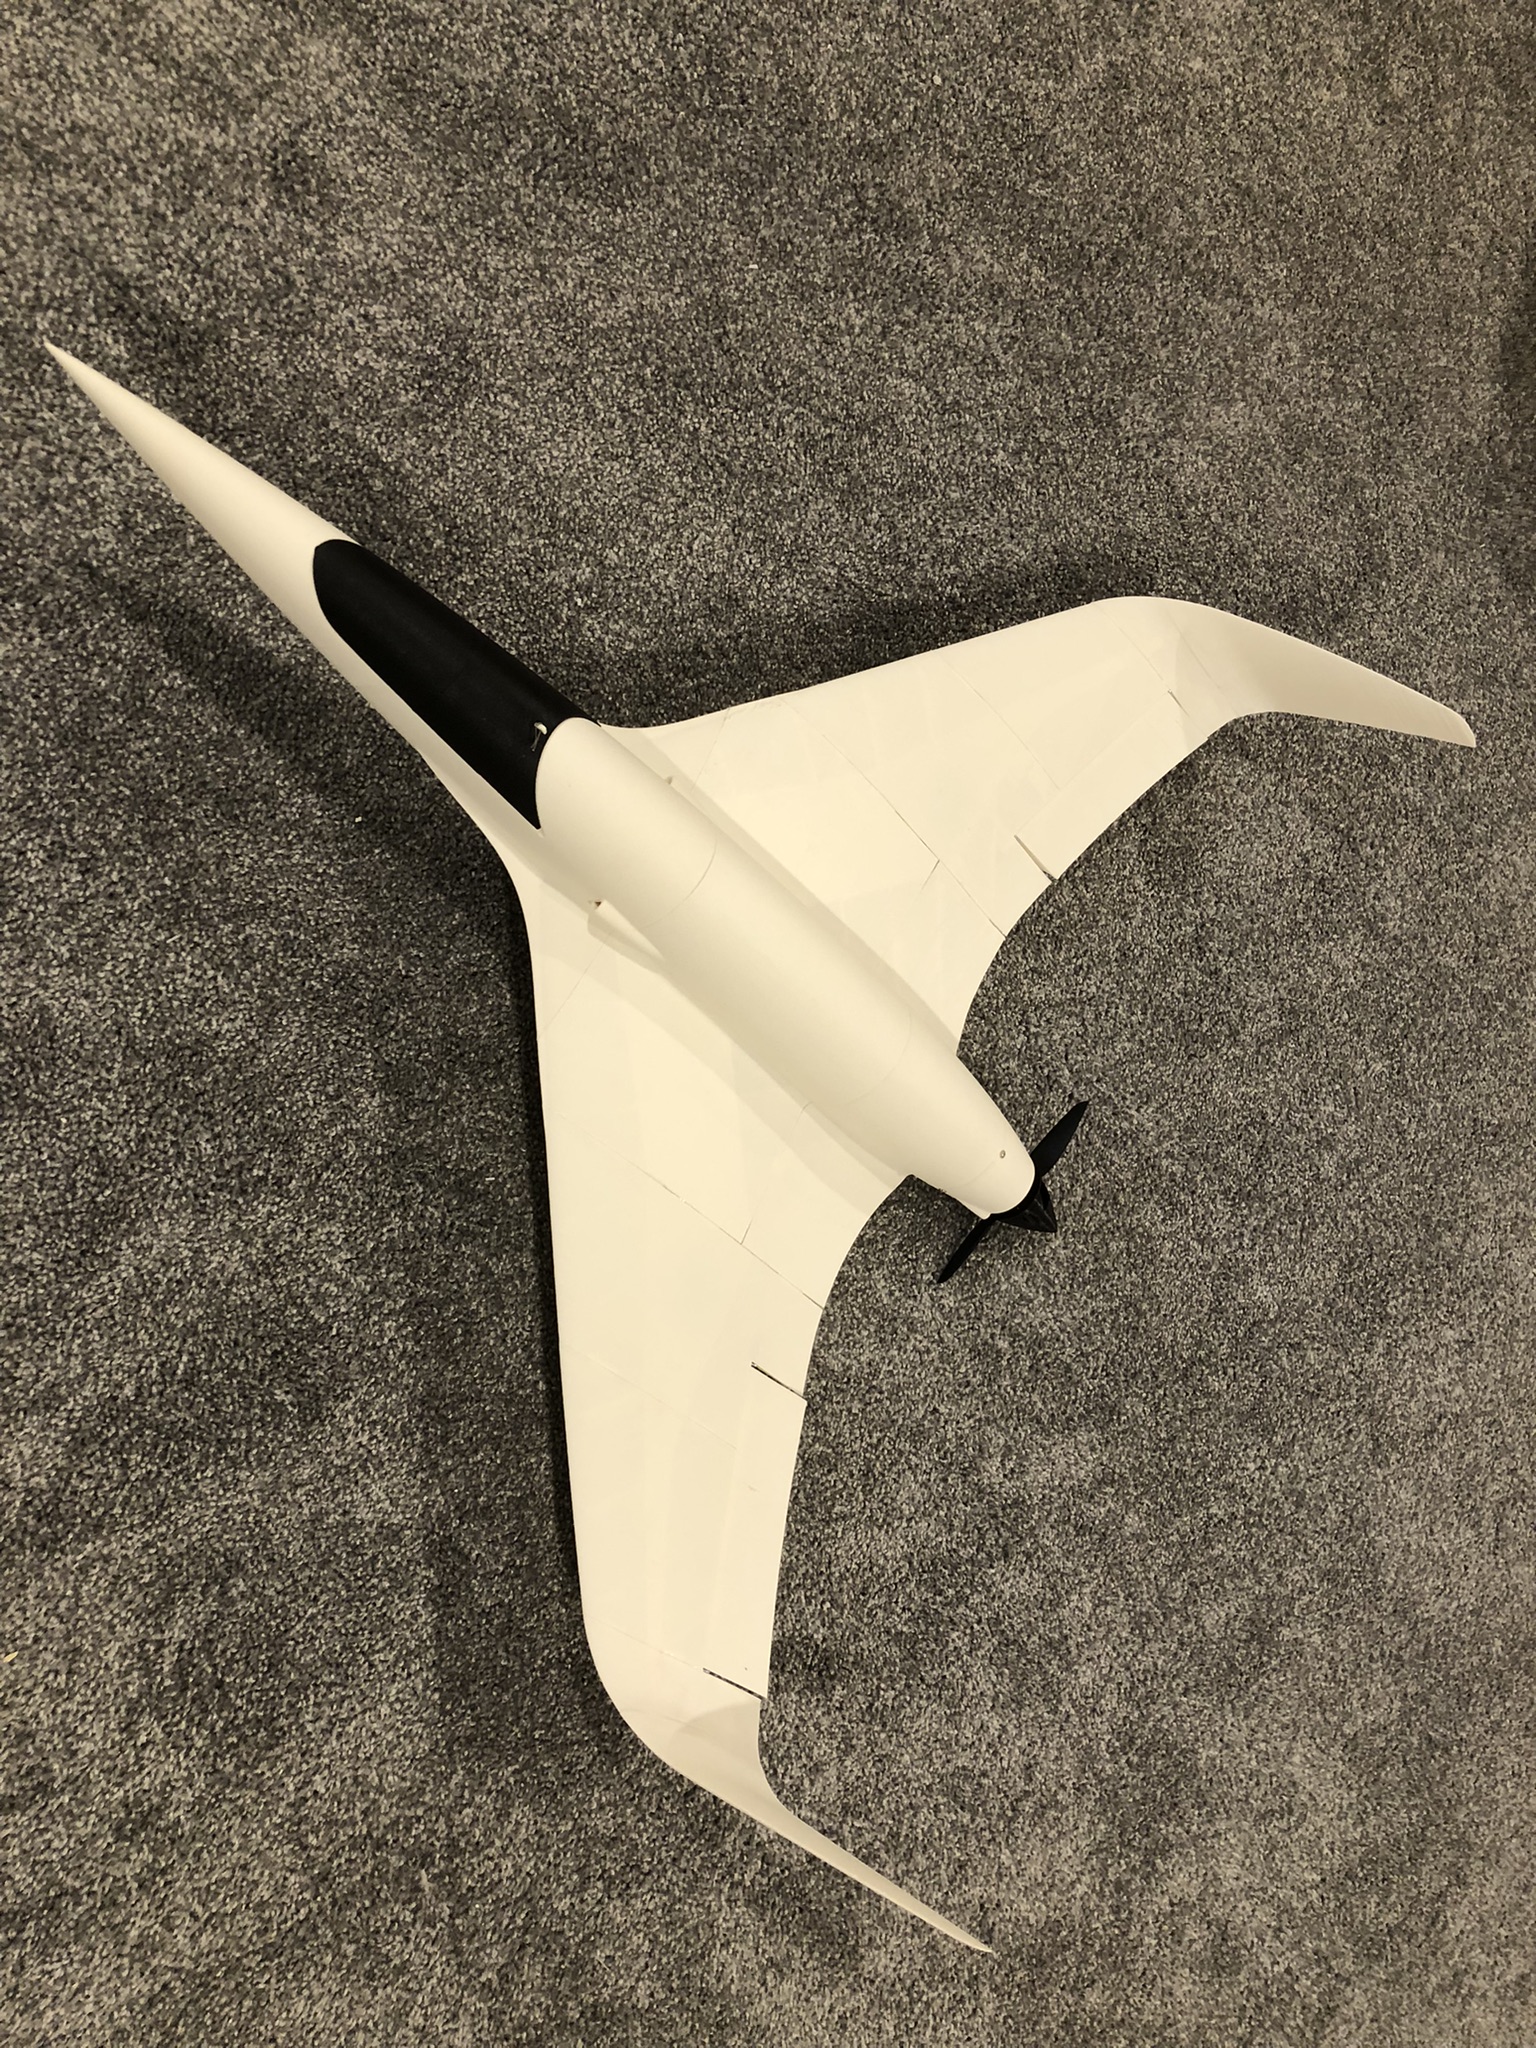
Plz don’t hit somebody with that! 😂Eclipson greywing out of lw-pla ready to go.
View attachment 213445

FlyerInStyle
Master member
Now Thats amazing!Eclipson greywing out of lw-pla ready to go.
View attachment 213445

Matagami Designs
Master member
Maidend my F-82 today! Had a good head wind so I think that helped with the weight. Can't wait to get more flight time. Till then I think some paint is in order.
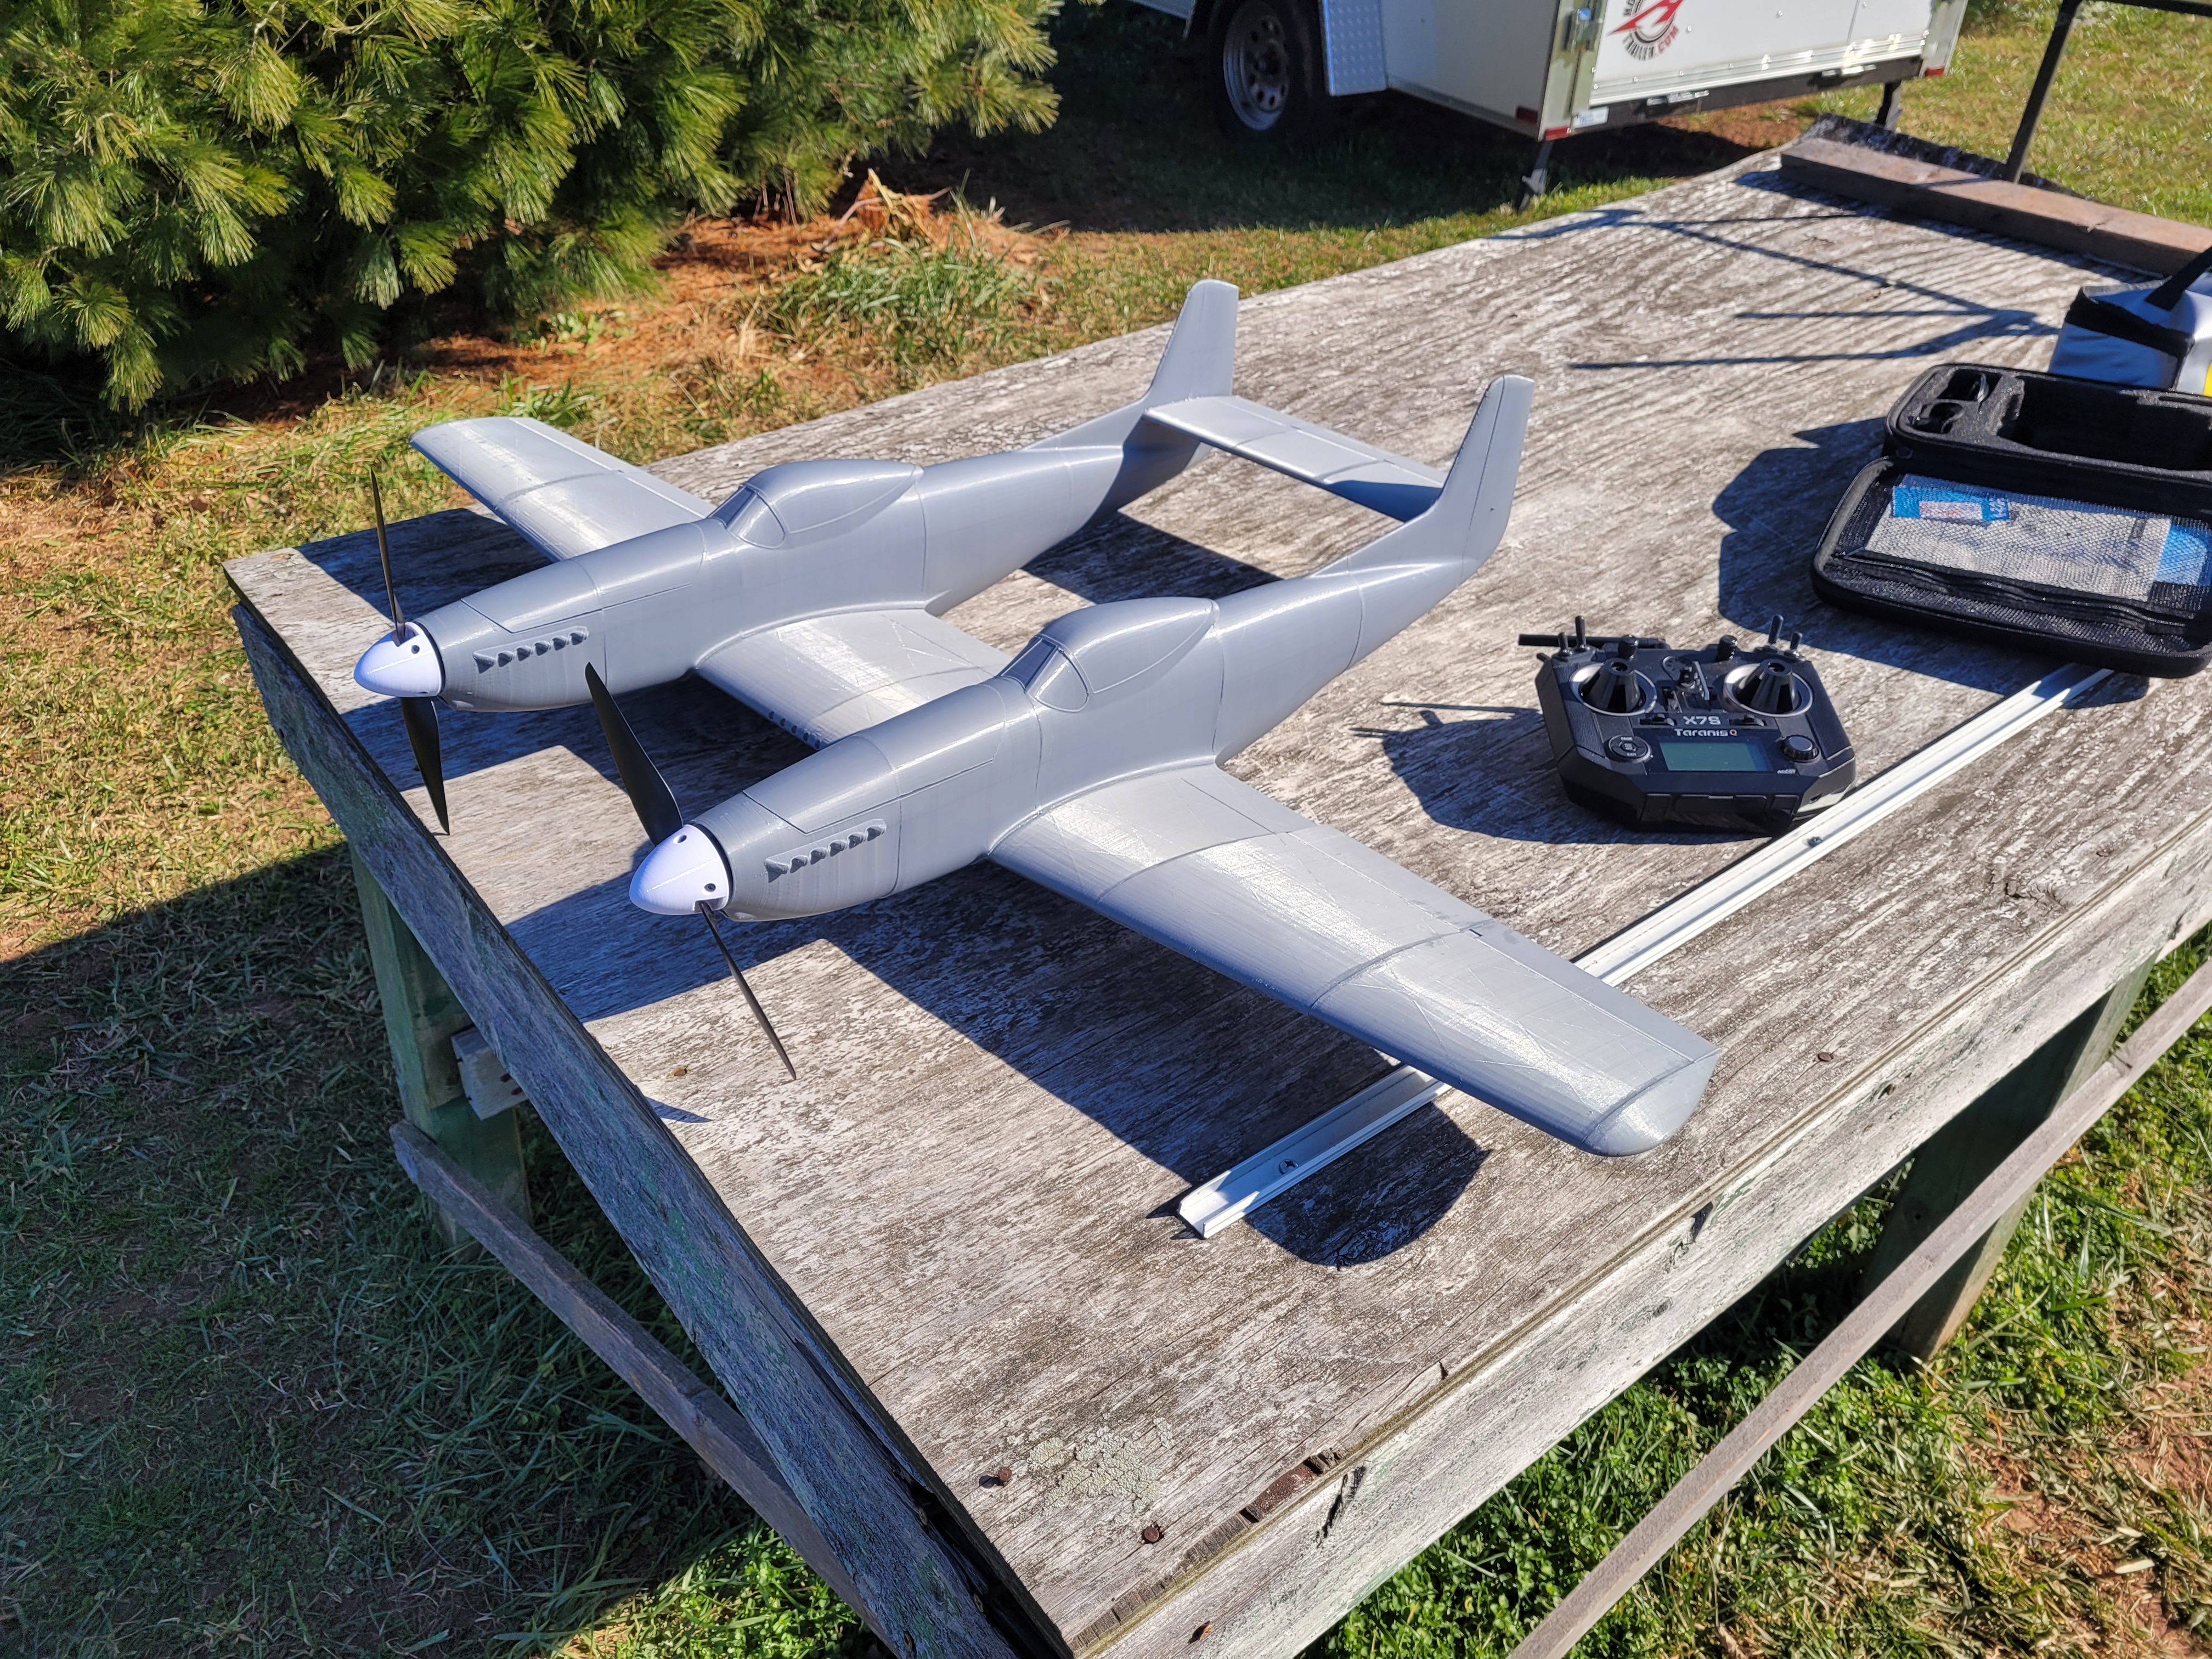
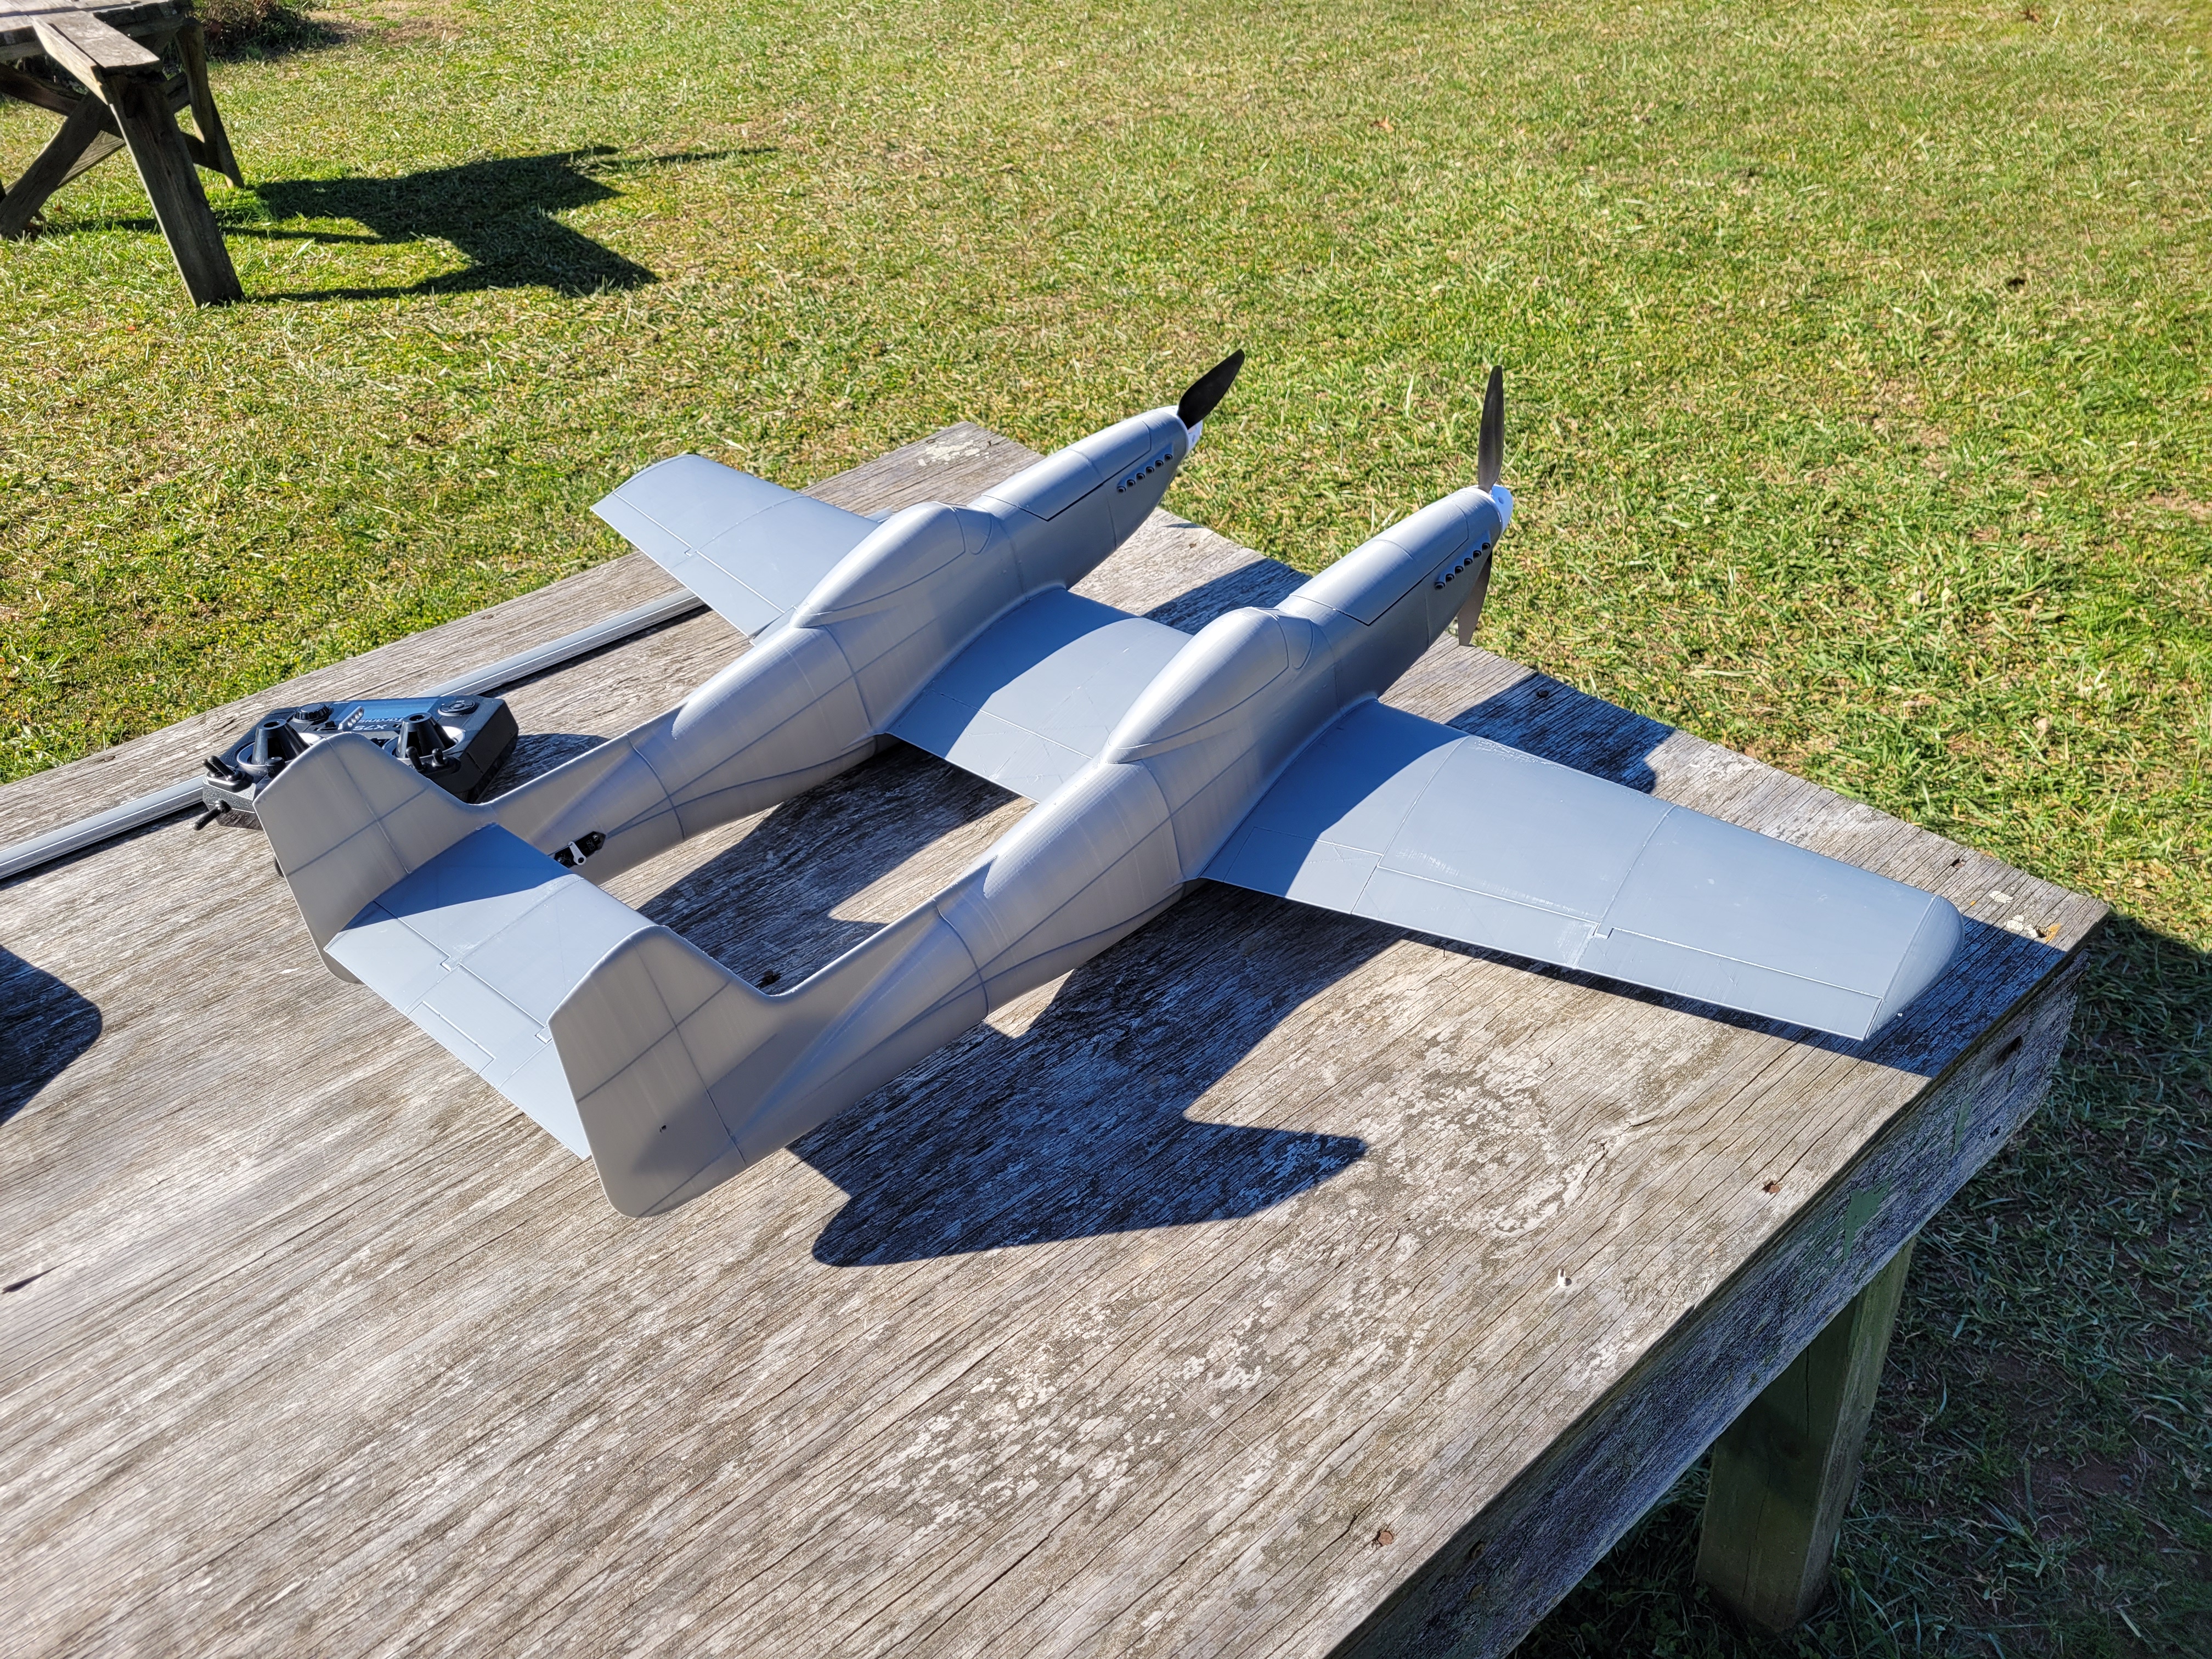

I have the EDF version in the works....Eclipson greywing out of lw-pla ready to go.
View attachment 213445

Trashing the gcode files that came with the Eclipson Model S and re-slicing. There are a few things that can be improved on over the provided files.
LB
- Start/end point for layers should be internal somewhere where they can't be seen rather than on the outside where it looks like @#$%.
- Rotate the object so the fan blows in a direction that does not blow sideways across the fuselage, wings, or control surfaces. Fan direction can vary from printer to printer. I've adjusted to blow from bottom to top of fuselage parts, canopy will be from the top, and front to back of wing/control surfaces. Helps keep everything symmetric and minimize warping, especially at the top of tall parts.
- Adding PET-G profiles for a more durable build and for high temp parts. (ie motor mounts)
- Stock gcode files are for a smaller print bed and are not printing in center of bed. Adjusting to center of bed for more consistent first layer.
- Using vase mode for all "A" single wall shell parts. Gets rid of the ugly seam that happens when the layer changes with non-vase mode.
- Lowered fan speed to reduce warping. Fan was distorting some parts when printing overhaning/bridging parts... (ie around the canopy opening for the fuselage.
LB
Keno
Well-known member
Do have Cura? Do most of my printing with it. Don't know about your printer for Cura if you check on PlanePrint there is setup chart that works pretty well. Also, LabPrint has a video for Prusa's slicer program settings that may be of value to you.Trashing the gcode files that came with the Eclipson Model S and re-slicing. There are a few things that can be improved on over the provided files.
- Start/end point for layers should be internal somewhere where they can't be seen rather than on the outside where it looks like @#$%.
- Rotate the object so the fan blows in a direction that does not blow sideways across the fuselage, wings, or control surfaces. Fan direction can vary from printer to printer. I've adjusted to blow from bottom to top of fuselage parts, canopy will be from the top, and front to back of wing/control surfaces. Helps keep everything symmetric and minimize warping, especially at the top of tall parts.
- Adding PET-G profiles for a more durable build and for high temp parts. (ie motor mounts)
- Stock gcode files are for a smaller print bed and are not printing in center of bed. Adjusting to center of bed for more consistent first layer.
- Using vase mode for all "A" single wall shell parts. Gets rid of the ugly seam that happens when the layer changes with non-vase mode.
- Lowered fan speed to reduce warping. Fan was distorting some parts when printing overhaning/bridging parts... (ie around the canopy opening for the fuselage.
LB
Last edited:
I mostly use Simplify3D. Every now and then I play with others looking for "new" ways to do things, but end up sticking with what I got a long time ago.Do have Cura? Do most of my printing with it. Don't know about your printer for Cura if you check on PlanePrint there is setup chart that works pretty well. Also, LabPrint has a video for Prusa's slicer program settings that may be of value to you.
Keno
Well-known member
Good program to use, I have it also. Kind of curious on the print bed you using & it appears to be smaller than your actual printing surface sheet & curious of its make. Can you control its temp at 60C? if so, here is a way to make things stick. Spay it a coating of air spay (Aqua Net) bake it on until cured, do this 3 times. Then before print spay again & print. For next print scape off any unsmooth areas & spray & print next piece. Cleaning plate of spray is by coating it with alcohol, then wash it off. This may help with base warping problems. Stay with it as it's a learning curve.I mostly use Simplify3D. Every now and then I play with others looking for "new" ways to do things, but end up sticking with what I got a long time ago.
KJ
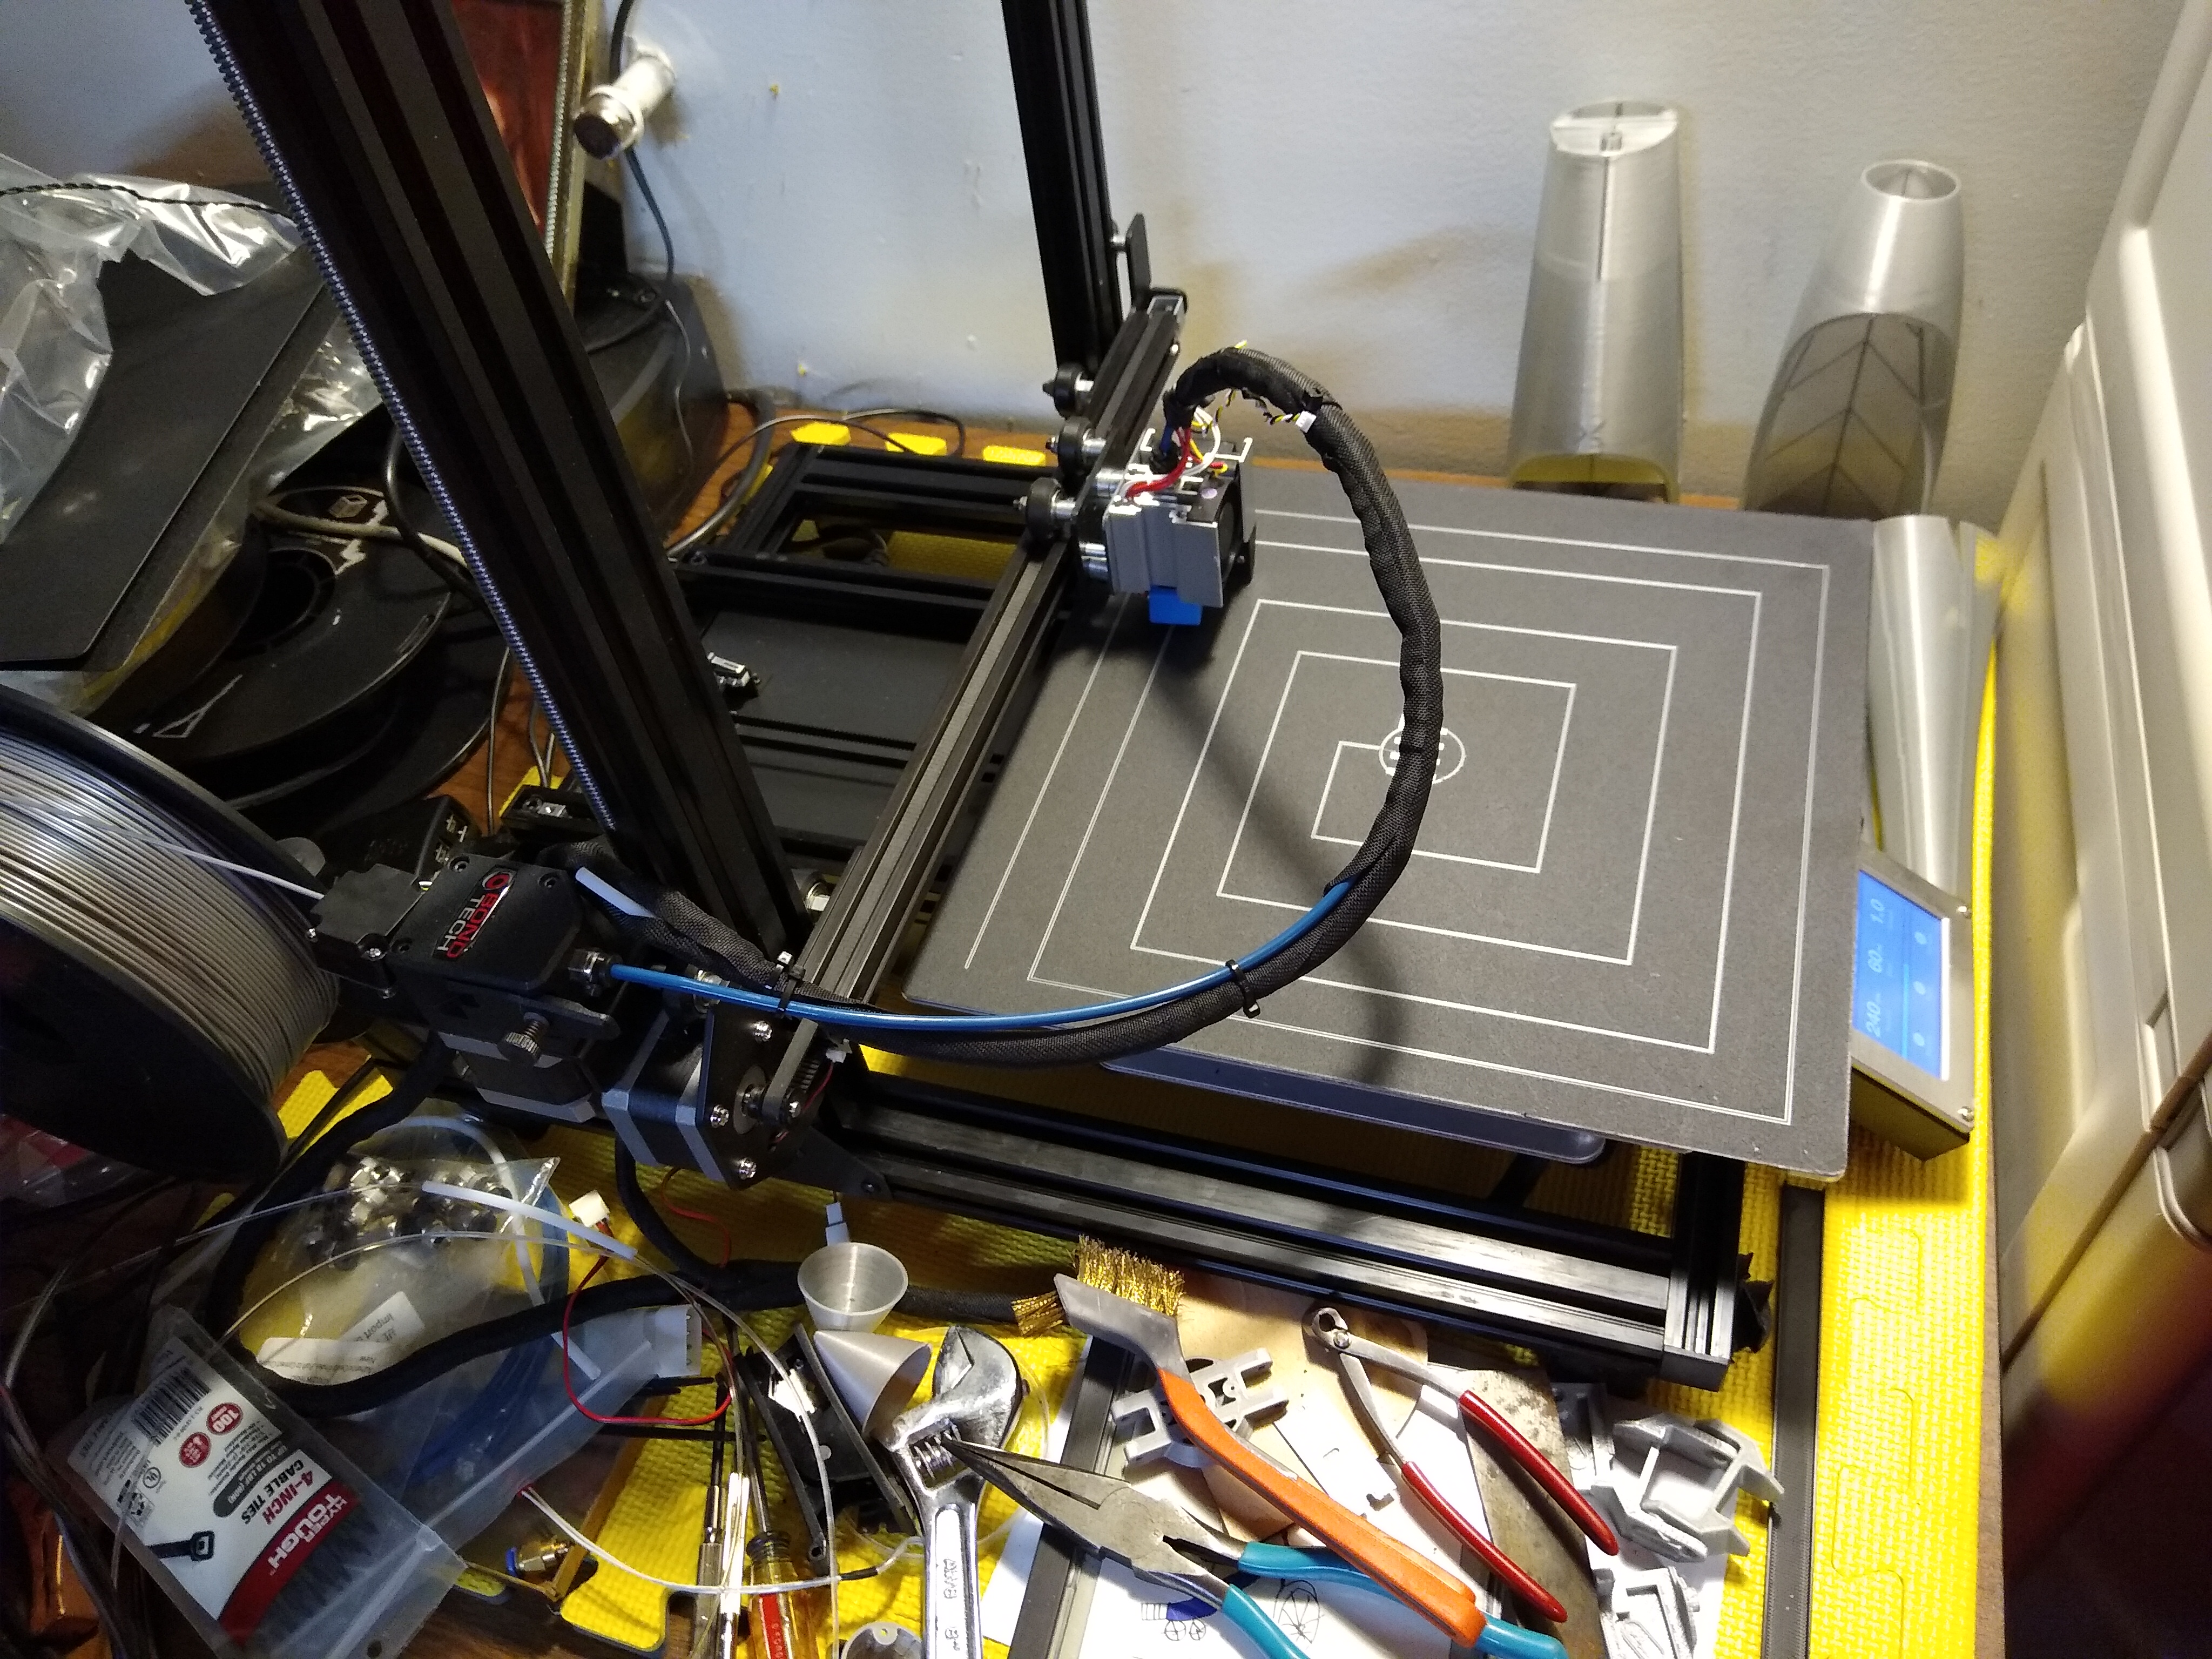
No need for hair spray. It's already coated and has good adhesion. 300x300 Monoprice MP10 magnetic mount heated bed. The warping happens on tall prints, with certain materials, on high overhang situations. The previous layers can move a bit from the cooling fan blowing on them causing the warping, not from parts lifting off the bed.Good program to use, I have it also. Kind of curious on the print bed you using & it appears to be smaller than your actual printing surface sheet & curious of its make. Can you control its temp at 60C? if so, here is a way to make things stick. Spay it a coating of air spay (Aqua Net) bake it on until cured, do this 3 times. Then before print spay again & print. For next print scape off any unsmooth areas & spray & print next piece. Cleaning plate of spray is by coating it with alcohol, then wash it off. This may help with base warping problems. Stay with it as it's a learning curve.
KJ
Been printing 6+years with "cheap" printers, so I have had plenty of learning opportunites. My XYZ has a glass bed which required the glue/hairspray till I got a good layer of kapton tape on it. Have not had to use any of that as long as bed alignment and first layer squish are set correctly. No more wasting time painting and cleaning the bed.
LB
Keno
Well-known member
Good program to use, I have it also. Kind of curious on the print bed you using & it appears to be smaller than your actual printing surface sheet & curious of its make. Can you control its temp at 60C? if so, here is a way to make things stick. Spay it a coating of air spay (Aqua Net) bake it on until cured, do this 3 times. Then before print spay again & print. For next print scape off any unsmooth areas & spray & print next piece. Cleaning plate of spray is by coating it with alcohol, then wash it off. This may help with base warping problems. Stay with it as it's a learning curve.
KJ
Sounds good. On tall prints such as control, tail & tall thin parts i use a vertical triangle brace support to help with vertical print distortion. been printing about same time. What is great about it every day you learn something new. Now printing a PlanePrint Big Bobber looks like going come out looking good. Take care & print on..No need for hair spray. It's already coated and has good adhesion. 300x300 Monoprice MP10 magnetic mount heated bed. The warping happens on tall prints, with certain materials, on high overhang situations. The previous layers can move a bit from the cooling fan blowing on them causing the warping, not from parts lifting off the bed.
Been printing 6+years with "cheap" printers, so I have had plenty of learning opportunites. My XYZ has a glass bed which required the glue/hairspray till I got a good layer of kapton tape on it. Have not had to use any of that as long as bed alignment and first layer squish are set correctly. No more wasting time painting and cleaning the bed.
LB
FlyerInStyle
Master member
I just wanted yo ask, I wanted to get a resin 3d printer and wanted to ask if anyone here uses them. Also what are the benefits of fdm vs. Sla?
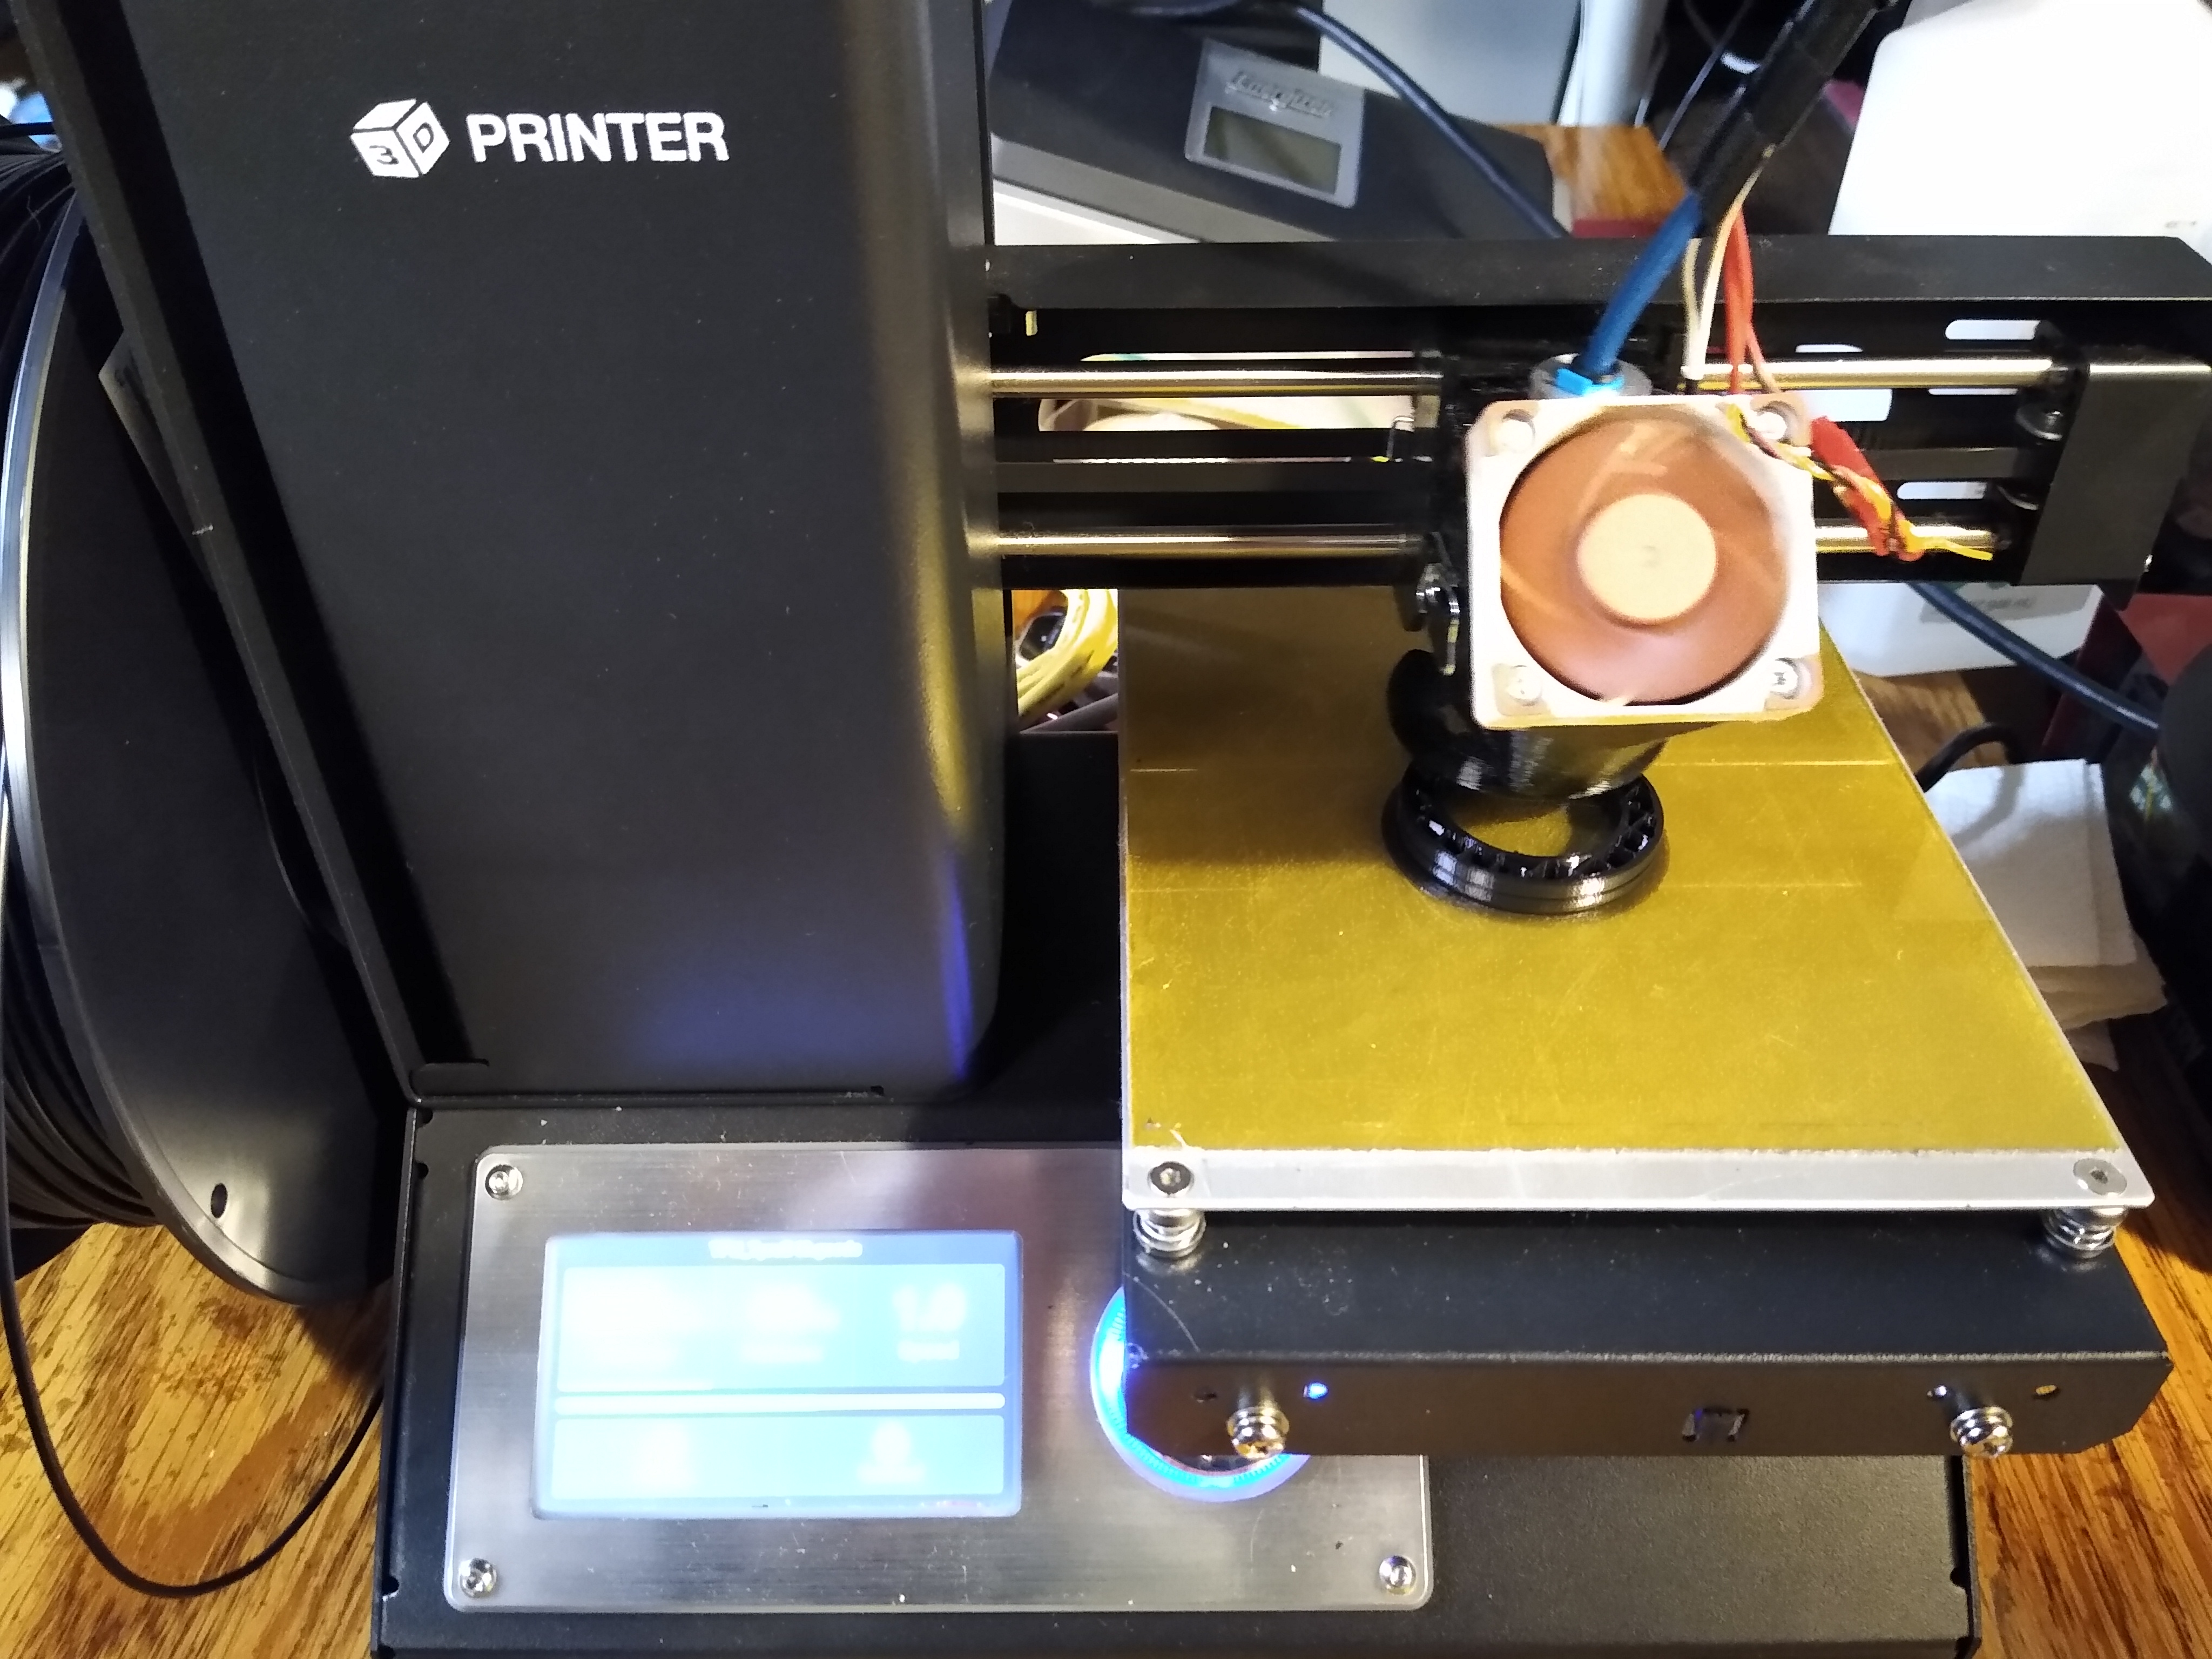
Bah. been trying to figure out what was going on with the MP Select mini. Had some underextrusion problems. Turned out the blockage was in the heat break. Probably caused by over retraction lifting soft filament up into the cool part of the break. Got it all cleaned out and am printing TPU tires for the Eclipson Model S.
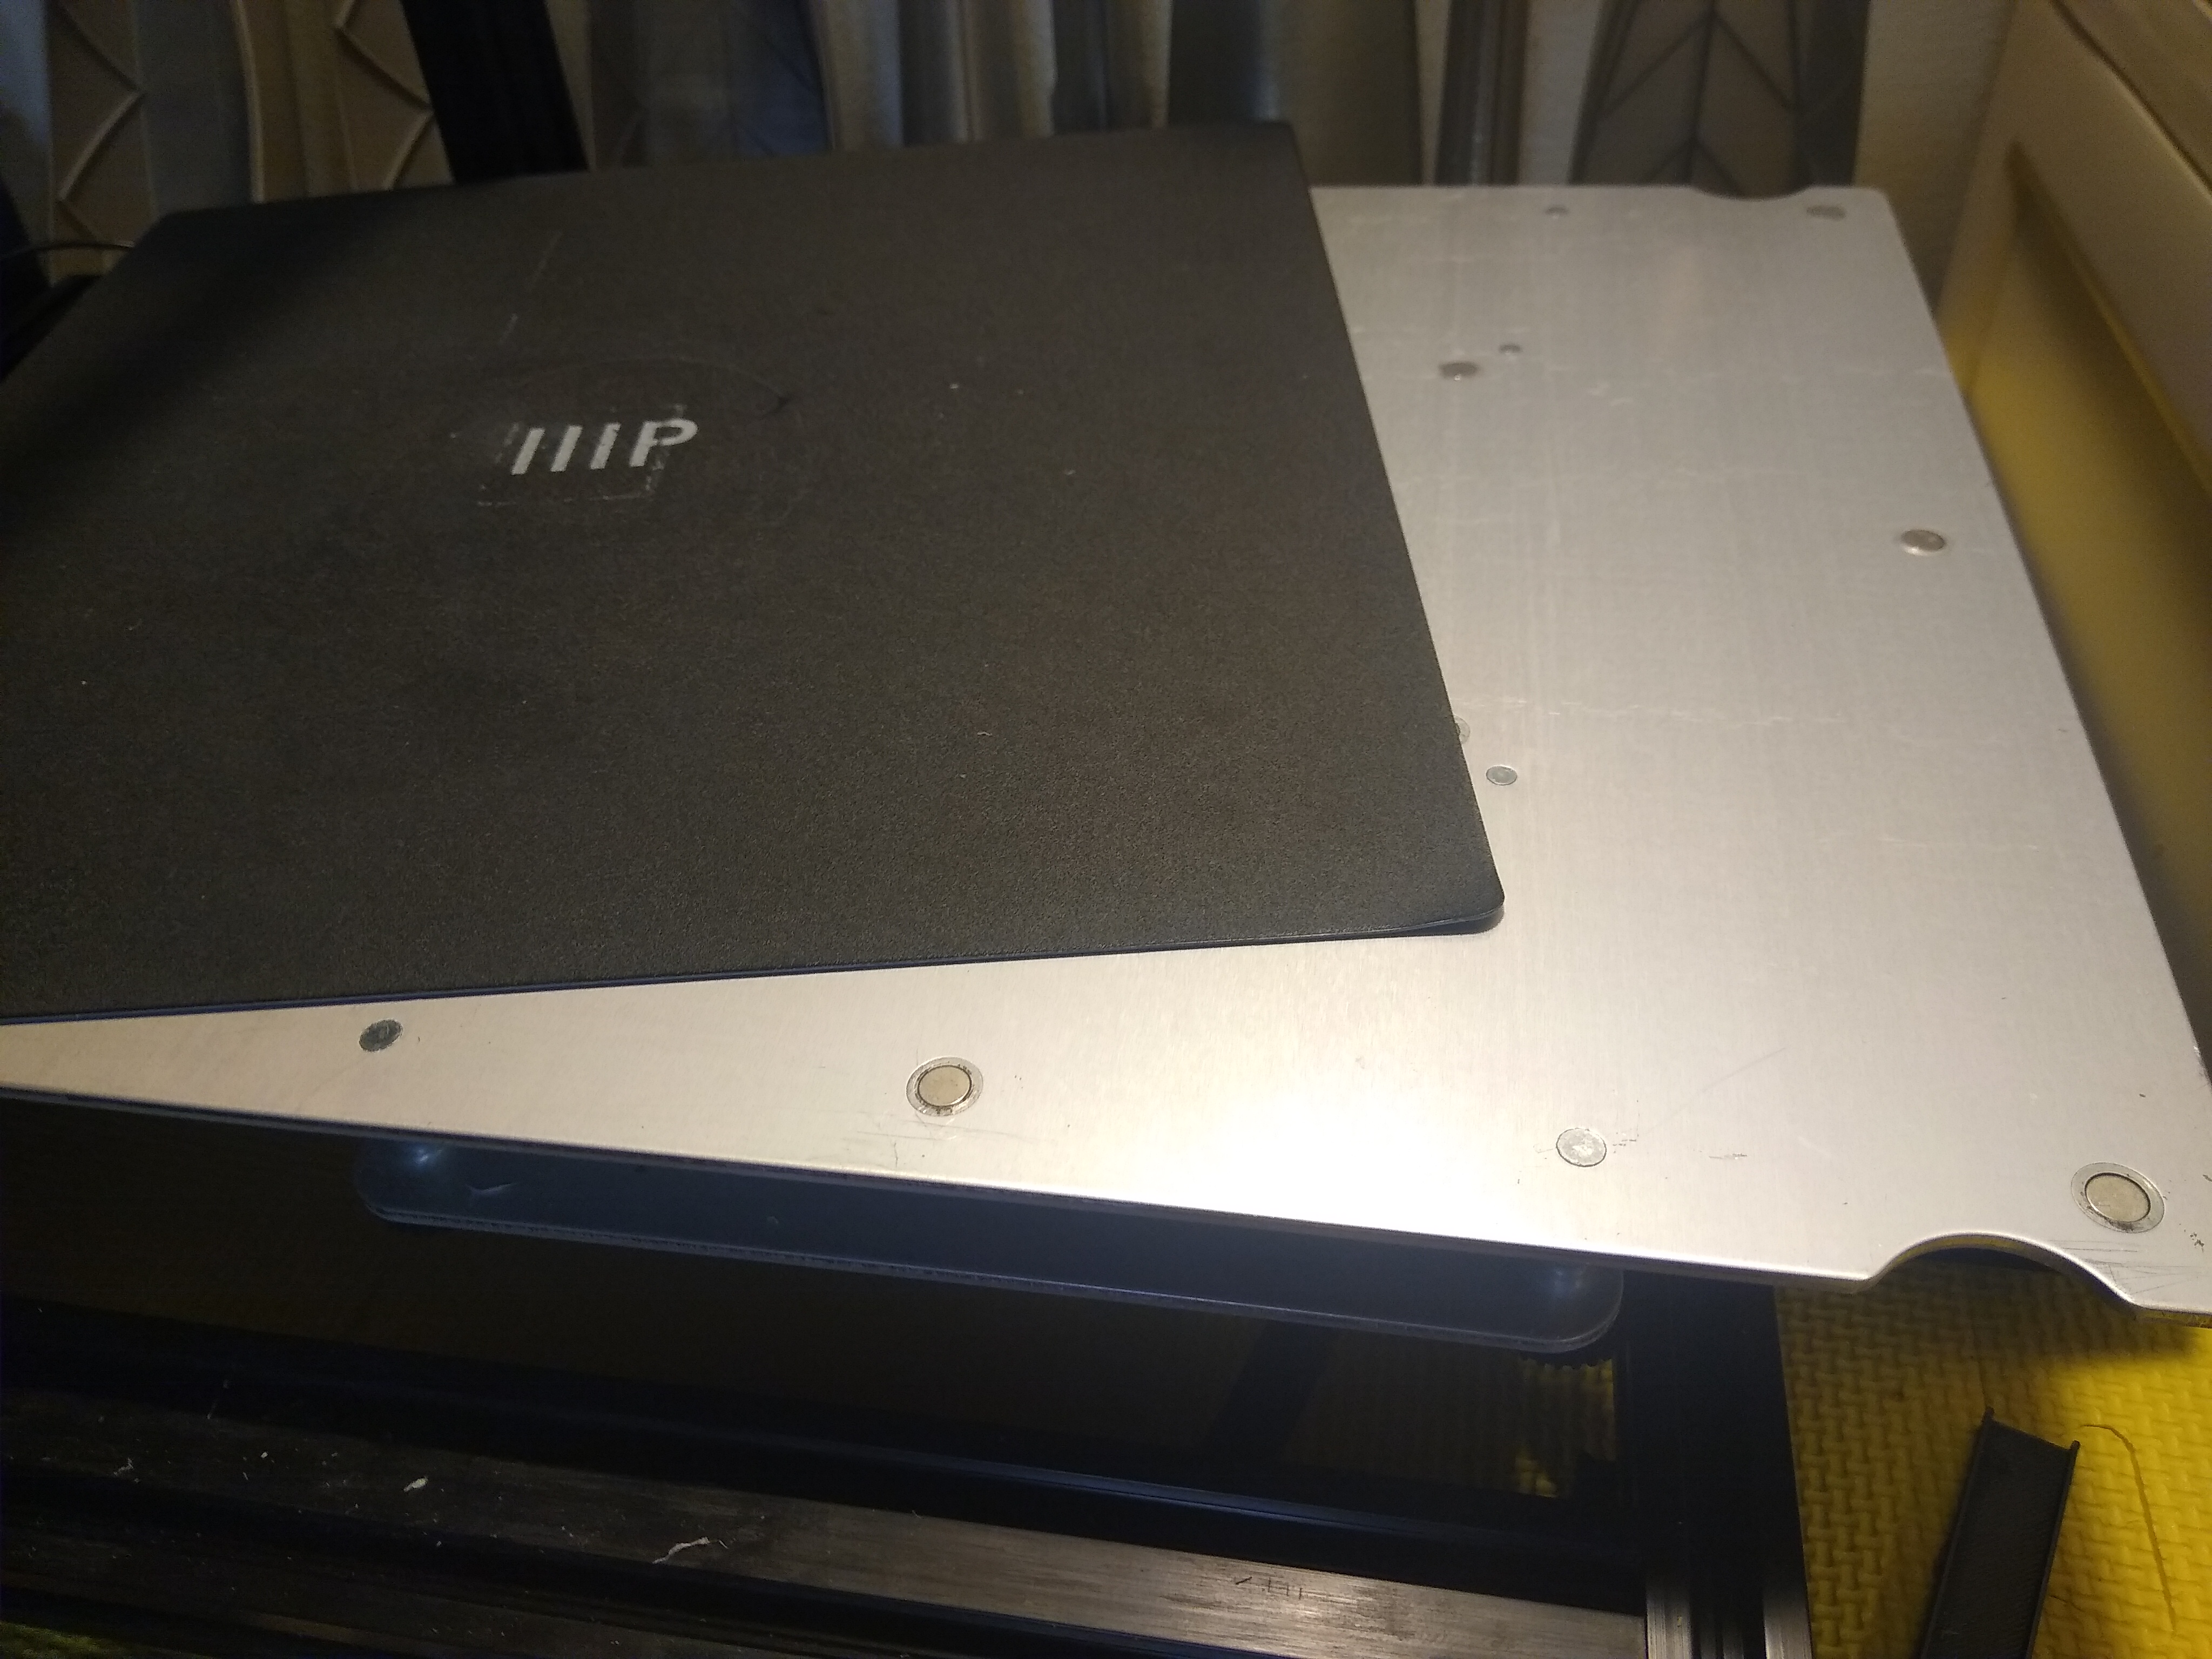
The magnetic Heated bed on the MP10 is 300x300 just like the removeable plate. The adjustment screw plate is smaller which probably made it look like the heated bed is smaller. Shifted the plate over so you can see all 3 plates
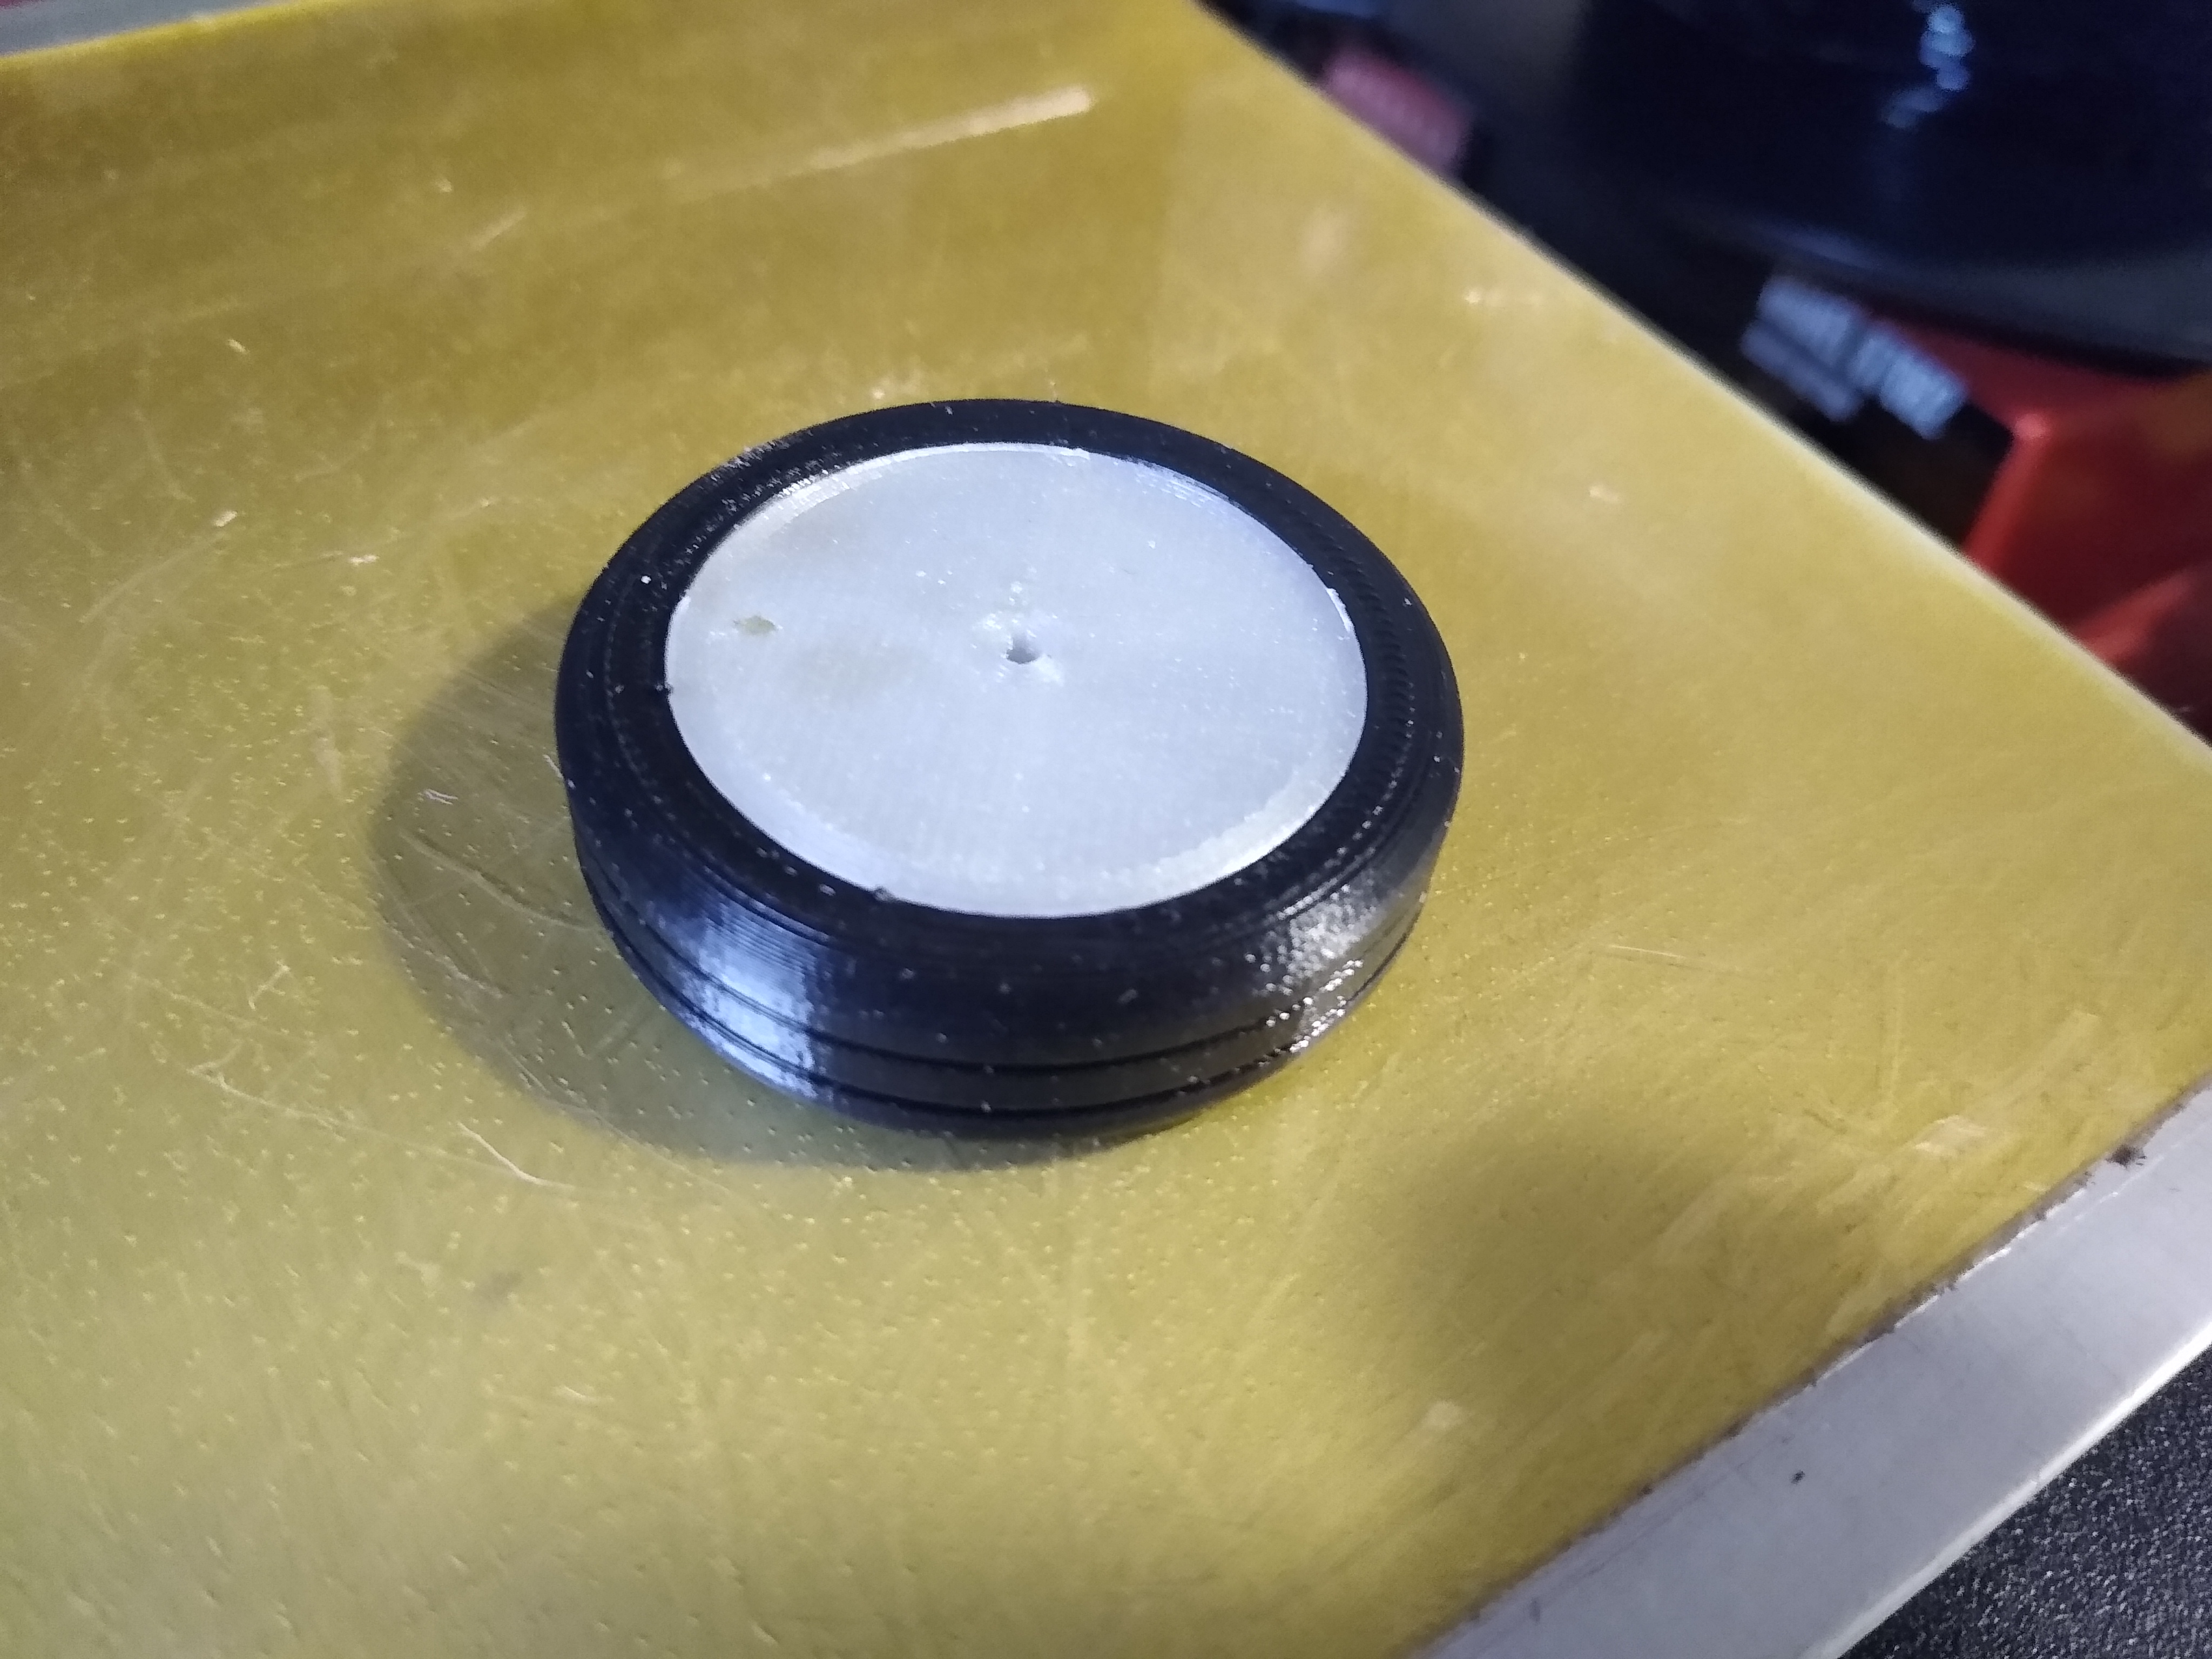
Tire completed and mounted on rim.
The magnetic Heated bed on the MP10 is 300x300 just like the removeable plate. The adjustment screw plate is smaller which probably made it look like the heated bed is smaller. Shifted the plate over so you can see all 3 plates
Tire completed and mounted on rim.
Last edited:
I just wanted yo ask, I wanted to get a resin 3d printer and wanted to ask if anyone here uses them. Also what are the benefits of fdm vs. Sla?
Resin printers generally have small volume build area, but very high detail. They are a completely different beast that I have not yet decided to play with. Too much cleaning and potential for spillage for this clumsy old fool. LOL
SLA printers have their place, but if you are thinking about printing planes, stick to a traditional FDM. Material and color choice variety is much greater with FDM.
You know, I thought the same thing when it first came out. Lawn Jarts FTW!Plz don’t hit somebody with that! 😂
FlyerInStyle
Master member
oh. I wanted to build sturdy reinforcements like motor mounts for rc planes, without the layer splitting problems, and I also found sla cheaper. that is why I was asking. I really want to stick wwith dtfb for building the actual plane for now though.Resin printers generally have small volume build area, but very high detail. They are a completely different beast that I have not yet decided to play with. Too much cleaning and potential for spillage for this clumsy old fool. LOL
SLA printers have their place, but if you are thinking about printing planes, stick to a traditional FDM. Material and color choice variety is much greater with FDM.
Similar threads

- Replies
- 2
- Views
- 632

- Replies
- 58
- Views
- 14K

- Replies
- 3
- Views
- 1K

- Replies
- 19
- Views
- 2K
- Replies
- 360
- Views
- 31K
